
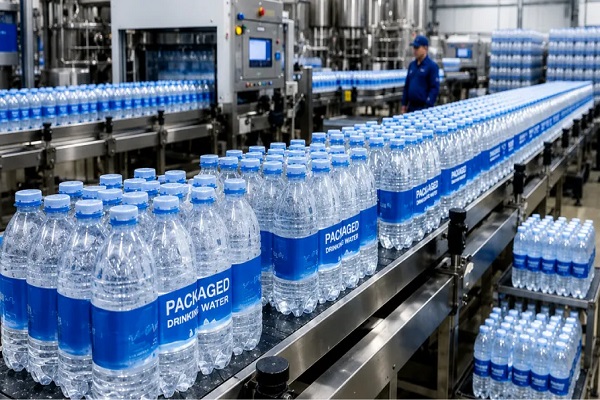
Entering the packaged drinking water industry requires more than a reliable source of clean water. Businesses also need organized processing, accurate filling, hygienic handling, and dependable packaging operations. A Mineral Water Bottling Plant brings these essential activities together, allowing manufacturers to produce bottles efficiently while maintaining consistent standards. As demand grows across retail stores, offices, restaurants, hotels, and travel destinations, suitable machinery can help businesses manage orders without unnecessary operational pressure. FREEION Engineering provides equipment solutions designed to support commercial production requirements, helping entrepreneurs establish organized facilities and prepare for long-term growth in the bottled water market.
Machinery That Supports Consistent Output
Production efficiency depends on how smoothly each stage operates. From water treatment and storage to bottle filling and sealing, every process needs appropriate equipment and coordination. A well-configured Mineral Water Bottling Plant helps manufacturers reduce manual handling, maintain organized workflows, and achieve more predictable production cycles.
Automation can also improve the consistency of filling operations. When machines control bottle positioning, liquid volume, and movement between stations, operators can manage production with greater accuracy. Consequently, businesses may reduce avoidable wastage and use their working hours more effectively. Selecting suitable machinery according to bottle sizes and daily targets is therefore an important decision.
Important Features for Daily Manufacturing
When purchasing equipment, manufacturers should examine machine construction, operating speed, maintenance requirements, and compatibility with their packaging materials. A Mineral Water Bottling Plant should be easy to operate and convenient to clean, especially when production runs take place throughout the day.
Stainless steel contact surfaces, practical controls, and dependable components can support hygienic operations. Furthermore, accessible machine parts simplify inspection and routine servicing. Buyers should also review installation requirements, electrical consumption, available floor space, and operator training before finalizing their purchase.
Improving Packaging Efficiency Across Production
Packaging is an important part of the customer’s experience because bottles must remain sealed, identifiable, and ready for transportation. Efficient packaging arrangements help businesses organize finished products, reduce handling difficulties, and prepare dispatches on time.
A suitable Mineral Water Bottling Plant can coordinate filling, capping, and packaging activities to support a steady workflow. Manufacturers can also choose equipment based on bottle shapes, sizes, and packaging designs. This flexibility becomes valuable when businesses serve different distributors or introduce new product formats. Proper coordination between machines helps prevent bottlenecks and keeps daily operations more manageable.
Mineral Water Bottling Plant Choosing Capacity for Your Business Needs
Production capacity should reflect realistic sales forecasts rather than ambitious estimates alone. Small businesses may begin with moderate output, while established suppliers require faster lines to serve multiple markets. Comparing machine specifications helps buyers select a configuration that fits their business model. A Mineral Water Bottling Plant that matches actual demand can support better resource planning and make future upgrades easier.
A Mineral Water Bottling Plant needs regular inspections. Before placing an order, discuss production speed, bottle dimensions, automation level, and servicing arrangements with the supplier. Clear technical information helps prevent mismatched expectations. Also, consider whether the layout leaves room for additional equipment as sales increase. Thoughtful selection can protect the investment and improve daily productivity.
Labeling and Product Presentation
Labels communicate product information and help packages stand out on shelves. They must be applied neatly, consistently, and in a way that suits the bottle design. Reliable labeling equipment can reduce alignment issues and help maintain a professional appearance during high-volume runs.
Businesses exploring a Hot Melt Glue Roll Fed Labeling Machine can consider how roll-fed labels, adhesive application, and machine speed fit their packaging requirements. This equipment is useful to evaluate alongside bottle shape, label material, and production volume, so the chosen arrangement supports the overall packaging line without creating delays.
Maintenance and Operator Practices
Regular maintenance keeps machinery dependable and can prevent avoidable downtime. Operators should follow cleaning schedules, inspect moving parts, check connections, and report unusual sounds or performance changes. Keeping spare wear components available may also help restore operations quickly when servicing is needed.
Clean routines support Mineral Water Bottling Plant. Staff training is equally important. Employees who understand startup procedures, safe operation, shutdown routines, and basic troubleshooting can manage equipment confidently. In addition, written checklists encourage consistent practices across shifts and make supervision easier.
Working With FREEION Engineering
Equipment selection becomes easier when manufacturers receive clear guidance about their operational needs. FREEION Engineering can help businesses consider suitable machinery configurations, production expectations, and packaging requirements. Discussing intended output, bottle formats, available space, and future plans allows buyers to compare options more carefully.
A Mineral Water Bottling Plant can scale gradually. A Mineral Water Bottling Plant requires trained staff. Looking beyond the initial price helps buyers evaluate the long-term value of machinery, including service needs, operating efficiency, and expansion possibilities. Operators oversee this Mineral Water Bottling Plant.
Conclusion
Bottled water manufacturing requires coordinated processes, suitable technology, and consistent attention to quality. Choosing a Mineral Water Bottling Plant that matches production goals can help businesses improve workflow, manage packaging, and serve customers reliably. With careful planning, trained operators, and appropriate equipment from FREEION Engineering, manufacturers can build a dependable production setup and prepare their operations for sustainable growth.